- Company overview The heart of SMC Vision & Philsophy Partnership Certifications Company culture
- Our service Design and Engineering Maintenance and Service Examine Production Line Upgrade and Transformation Storage and Logistics Processing, Trading and Distributor
- Management Our history Global responsibility Info Center
- Procurement center Internship
- Metal Steel Products Stainless Steel Products Aluminum Products Copper Products Galvanized Steel and PPGI Special Alloy Building Material
- Containers ISO Standard Container Equipment Container Storage Container Tank Container Container Fittings Container Trailer Refrigerated/Reefer Container Offshore Container Container House
- Gas Cylinder & Fire Extinguisher Cryogenic Liquid Cylinder Oxygen Gas Cylinder Storage Tank CNG Gas Cylinder LPG Gas Cylinder Hydrogen Gas Cylinder Nitrogen Gas Cylinder Industry Gas Cylinder Fire Extinguisher
- Metal Machinery Motor Forming Machine Cutting Machine Processing Machine Bending Machine Block Machine Spare Parts Other Machinery
- Mechanical Products Conveyor Belt Miscellany Mooring Equipment Laser Equipment Bearing Marine Equipment Vehicle Industry Pressure Vessel
- Electrical System Transformer Production Line Lighting System Power Distribution Automation Electrical Cable Solar Power System Electric Protection System
- Project Plastic Pipes and Pipe Fittings Fiberglass Reinforced Plastic Pontoon System
High Speed Steel (HSS) Bar & Tool Steel Bar


Diameter: 1-500mm
Length: 1000-6000mm
Material: HSS, Tool Steel
Grade: M2, M35, M42, T1, T15, D2, D3, H13, O1, A2, S7, P20
Surface: Black, Peeled, Ground, Polished, Bright
Shanghai Metal Corporation is a leading High Speed Steel (HSS) Bar and Tool Steel Bar manufacturer and supplier.
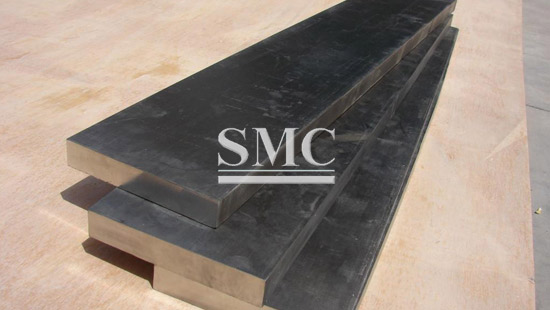
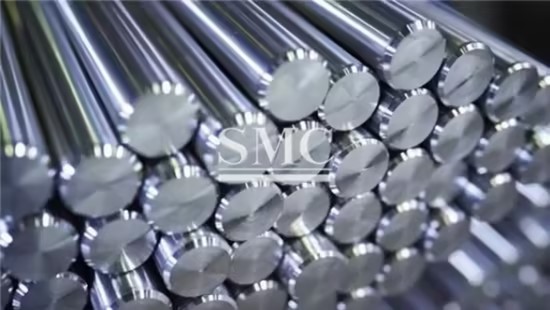
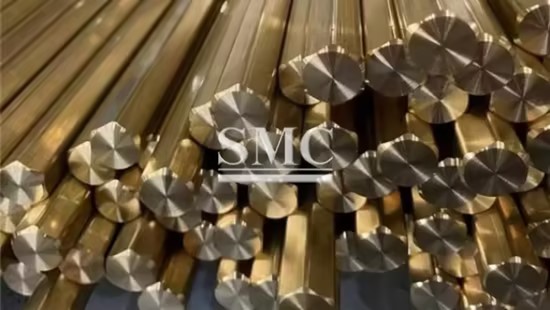
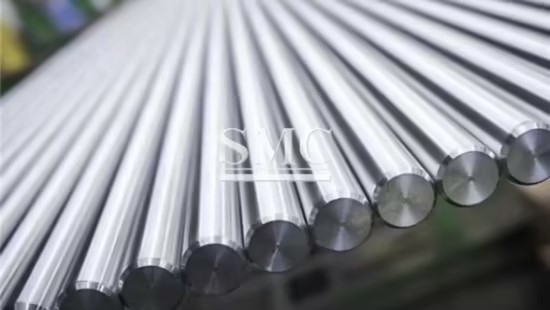
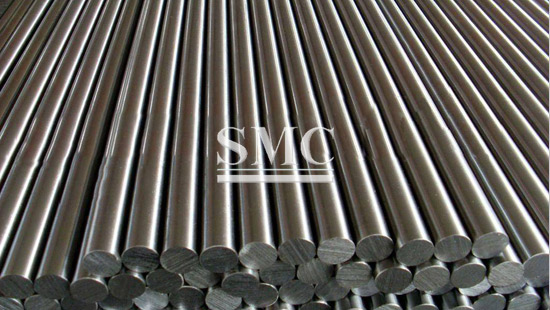
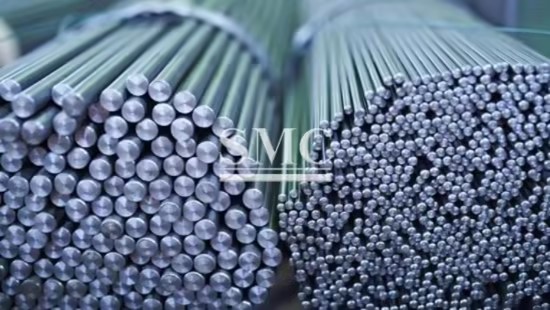
Our HSS bars and tool steel bars are solid steel bars supplied in round, square, flat, and hexagonal shapes. They are made from grades such as M2, M35, M42, T1, T15, D2, D3, H13, O1, A2, S7, and P20, with diameters from 1mm to 500mm and lengths from 1000mm to 6000mm. These bars are used to produce drills, taps, milling cutters, reamers, dies, punches, molds, and wear-resistant machine parts. They solve tooling and machining problems that require high hardness, wear resistance, red hardness, edge retention at elevated temperatures, and stable performance under repeated cutting or forming. Typical applications include tool and die making, mold manufacturing, automotive parts, aerospace components, machinery, and general metalworking. Surfaces can be black, peeled, turned, ground, polished, or bright, and custom sizes or cut lengths are available.
If you want to know more about our steel products or High Speed Steel (HSS) Bar and Tool Steel Bar price, please feel free to contact us, we will reply you within 24 hours.
-
1. Type: Solid high speed steel and tool steel bars.
2. Composition: HSS contains W, Mo, Cr, V, Co for red hardness and wear resistance; tool steel contains C, Cr, Mo, V, W and is divided into cold work, hot work, and plastic mold steel.
3. Structure: Round, square, flat, and hexagonal bars.
4. Function and Application: Round bars for cutting tools; square and flat bars for molds, punches, and tool blanks; hex bars for tool shanks and wrench parts.
5. Hardness and Standard: HSS HRC 62–66 after heat treatment; tool steel depends on grade and condition. ASTM, AISI, DIN, GB, JIS. Standard
-

-
-
1. High Red Hardness
Maintains hardness and edge strength at high cutting temperatures, enabling faster machining and fewer tool changes.
2. Excellent Wear Resistance
Resists abrasion during cutting, punching, and forming, extending tool and die life and reducing replacement costs.
3. Balanced Hardness and Toughness
Multiple grades offer different hardness and toughness combinations, helping prevent chipping and cracking in specific applications.
4. Consistent Material Quality
Uniform carbide distribution and stable heat treatment response provide predictable machining and hardening, reducing rejects and rework.
-
1. Metal Cutting Tools
For drills, taps, end mills, and reamers. HSS provides red hardness and edge retention at high cutting speeds. Recommended: M2, M35, M42, T15 round bars; ground or bright; HRC 62–66.
2. Cold Work Dies and Punches
For blanking, stamping, shearing, and cold forming. D2 and D3 resist wear; O1 and A2 balance wear and toughness; S7 resists shock.
-
Grade Contrast Table:
|
Tool Steel Round Bar |
Grade |
Size Rage |
|
|
DIN |
AISI |
||
|
1.2344 |
H13 |
15-580 mm |
|
|
1.2343 |
H11 |
15-505 mm |
|
|
1.2379 |
D2 |
15-380 mm |
|
|
1.2365A |
H10 |
15-450 mm |
|
|
1.2365B |
H10A |
15-450 mm |
|
|
1.2367 |
- |
15-450 mm |
|
|
1.2363 |
A2 |
15-300 mm |
|
|
1.2080 |
D3 |
15-200 mm |
|
|
1.2510 |
O1 |
15-300 mm |
|
|
1.2083 |
- |
15-300 mm |
|
|
1.2714 |
L6 |
15-350 mm |
|
|
1.2767 |
- |
15-300 mm |
|
|
1.2436 |
D6 |
15-130 mm |
|
|
Product |
Grade |
Size Rage |
|
|
DIN |
AISI |
||
|
Tool Steel Flat Bar |
1.2344 |
H13 |
Width: 300-810 mm Thickness: 14-120 mm |
|
1.2343 |
H11 |
Width: 300-810 mm Thickness: 14-120 mm |
|
|
1.2379 |
D2 |
Width: 300-810 mm Thickness: 14-100 mm |
|
|
1.2510 |
O1 |
Width: 300-810 mm Thickness: 14-100 mm |
|
|
1.2365 |
H10 |
Width: 300-810 mm Thickness: 14-100 mm |
|
|
1.2367 |
- |
Width: 300-810 mm Thickness: 14-100 mm |
|
|
1.2842 |
O2 |
Width: 300-810 mm Thickness: 14-100 mm |
|
|
1.2363 |
A2 |
Width: 300-810 mm Thickness: 14-100 mm |
|
|
1.2083 |
- |
Width: 300-810 mm Thickness: 14-100 mm |
|
|
1.2360 |
A8 |
Width: 300-810 mm Thickness: 14-100 mm |
|
|
1.2080 |
D3 |
Width: 300-600 mm Thickness: 14-80 mm |
|
Specification of High Speed Steel:
|
Specification of High Speed Steel |
||||
|
Product |
Grade |
Size Rage |
||
|
DIN |
AISI |
JIS |
||
|
HSS Round Bar |
1.3343 |
DINM2 |
- |
2.5-205 mm |
|
1.3243 |
M35 |
SKH51 |
2.5-160 mm |
|
|
1.3247 |
M42 |
SKH2 |
15-65 mm |
|
|
1.3346 |
M1 |
- |
2.5-205 mm |
|
|
1.3392 |
M52 |
- |
2.5-205 mm |
|
|
- |
M4 |
- |
15-80 mm |
|
|
- |
M7 |
SKH58 |
15-80 mm |
|
|
- |
W9 |
- |
3.6-160 mm |
|
|
HSS Square Bar |
1.3343 |
DINM2 |
- |
15-40 mm |
|
1.3244 |
M35 |
SKH59 |
15-40 mm |
|
|
1.2344 |
H13 |
SKD62 |
120-250 mm |
|
|
1.2367 |
- |
- |
120-180 mm |
|
|
HSS Flat Bar |
1.3343 |
M2 |
SKH51 |
With: 100-510 mm Thickness: 14-65 mm |
Chemical Composition of High Speed Steel:
|
Chemical Corporation of High Speed Steel (%) |
||||||||
|
Grade |
C |
Si |
Mn |
W |
Mo |
Cr |
V |
Others |
|
W9Mo3Cr4V |
0.77-0.87 |
0.20-0.40 |
0.20-0.40 |
8.50-9.50 |
2.70-3.30 |
3.80-4.40 |
1.30-1.70 |
- |
|
W6Mo5Cr4V2 |
0.80-0.90 |
0.20-0.45 |
0.15-0.40 |
5.50-6.75 |
4.50-5.50 |
3.80-4.40 |
1.75-2.20 |
- |
|
Din M2 |
0.86-0.94 |
≤0.45 |
≤0.40 |
6.00-6.70 |
4.70-5.20 |
3.80-4.50 |
1.70-2.00 |
- |
|
W6Mo5Cr4V2Al(M2Al) |
1.05-1.20 |
0.20-0.60 |
0.15-0.40 |
5.50-6.75 |
4.50-5.50 |
3.80-4.40 |
1.75-2.20 |
Al: 0.80-1.20 |
|
W6Mo9Cr4V2 |
0.97-1.05 |
0.20-0.55 |
0.15-0.40 |
1.40-2.10 |
8.20-9.20 |
3.50-4.00 |
1.75-2.20 |
- |
|
W6Mo5Cr4V2Co5(M35) |
0.88-0.96 |
0.25-0.45 |
0.20-0.40 |
6.00-6.70 |
4.70-5.20 |
3.80-4.50 |
1.70-2.00 |
Co: 4.50-5.50 |
|
W2Mo9Cr4VCo8(M42) |
1.05-1.15 |
0.15-0.65 |
0.15-0.40 |
1.15-1.85 |
9.00-10.00 |
3.50-4.25 |
0.95-1.35 |
Co: 7.75-8.75 |
|
W18Cr4V(W18) |
0.70-0.80 |
0.20-0.40 |
0.10-0.40 |
17.50-19.00 |
≤0.3 |
3.80-4.40 |
1.00-1.40 |
- |
|
W4Mo3Cr4VSi(W4) |
0.88-0.98 |
0.50-1.00 |
0.20-0.40 |
3.50-4.50 |
2.50-3.50 |
3.80-4.40 |
1.20-1.80 |
- |
|
W4Mo2Cr4VSi(T-4241) |
0.90-1.00 |
0.80-1.30 |
0.20-0.45 |
1.50-2.50 |
0.50-1.20 |
3.80-6.00 |
0.50-1.00 |
- |
|
H13(4CrMoSiV1) |
0.32-0.45 |
0.80-1.20 |
0.20-0.50 |
- |
1.10-1.75 |
4.75-5.50 |
0.80-1.20 |
- |
|
Cr12Mo1V1 |
1.40-1.60 |
≤0.60 |
≤0.60 |
- |
0.70-1.20 |
11.00-13.00 |
0.50-1.10 |
- |
|
3Cr2W8V |
0.30-0.40 |
≤0.40 |
≤0.40 |
7.50-9.00 |
- |
2.20-2.70 |
0.20-0.50 |
- |
|
9Cr18MoV |
0.85-0.95 |
≤0.80 |
≤0.80 |
- |
1.00-1.30 |
17.00-19.00 |
0.07-0.12 |
- |
|
9Cr18Mo |
0.95-1.10 |
≤0.80 |
≤0.80 |
- |
0.40-0.70 |
16.00-18.00 |
- |
- |
|
9Cr18 |
0.90-1.00 |
≤0.80 |
≤0.80 |
- |
≤0.75 |
17.00-19.00 |
- |
- |
Packaging of High Speed Steel:
Standard Packaging
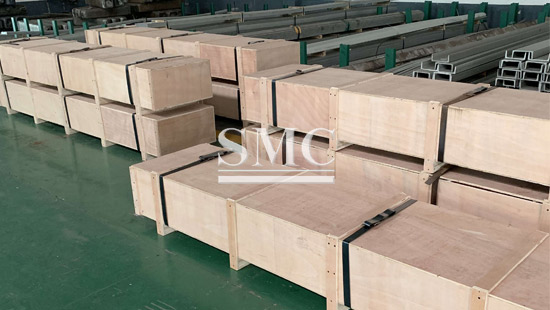
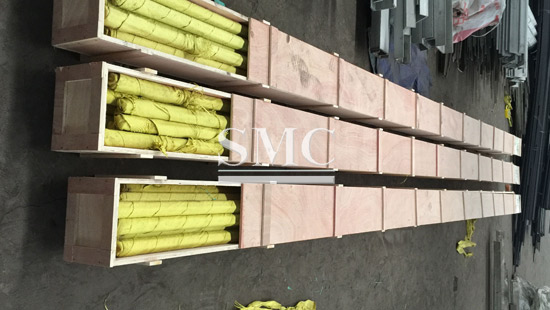
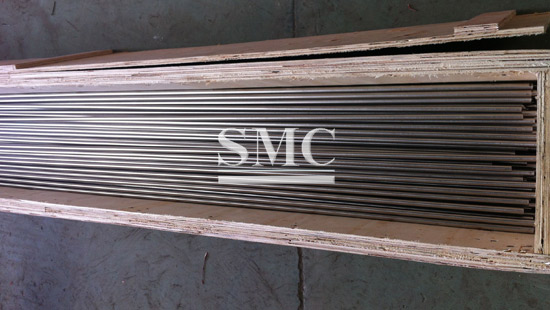
HSS and tool steel bars are cleaned, dried, and coated with anti-rust oil. Bar ends are fitted with plastic end caps. Bars of the same grade and size are bundled with steel straps. Each bundle is wrapped with anti-rust paper or VCI film, then packed in fumigated wooden boxes or on wooden pallets.
Shipping
We support FCL and LCL sea freight, air freight, and express delivery depending on order quantity and destination.
Trade terms: EXW / FOB / CIF. Other terms may be available upon request.
Shipping costs are calculated based on total gross weight, volume, destination, and selected transportation method.
Lead Time
Samples: 3–7 working days
Standard orders: 15–25 working days
Customized orders: 25–40 working days
Q. What information do you need for a custom quotation?
A. Please provide: Grade, Shape (Round/Square/Flat/Hex), Diameter/Thickness, Length, Surface Finish, Hardness/Heat Treatment, Quantity, Tolerance, Standard, Destination Port, and Trade Term.
Q. What is the MOQ and production lead time?
A. MOQ is typically 500 kg per grade/size. Custom melting or special sizes: 1,000 kg. Lead time is 15–25 days for standard orders and 25–40 days for customized orders after deposit or original L/C.
Q. What quality standards and certificates are available?
A. Products comply with ASTM A600/A681, DIN 1.3343/1.2379/1.2344, GB/T 9943, and JIS G4403. Mill test certificate EN 10204 3.1, ISO 9001, and third-party inspection (SGS, BV) are available.
Q. How long does sample preparation take?
A. 3–7 working days for standard grades/sizes with simple cutting. 10–15 working days for custom diameter, length, surface, or heat treatment. Sample quantity: 1–5 pieces or 5–20 kg.
Q. How do I choose between HSS and tool steel for my application?
A. Choose HSS for cutting tools (drills, taps, end mills) requiring red hardness and edge retention at high cutting temperatures. Choose tool steel for cold work dies, hot work dies, plastic molds, punches, and wear-resistant parts.
Q. Which HSS grade should I use for stainless steel, titanium, or high-strength alloys?
A. M2 for general steel; M35 for stainless steel and higher heat resistance; M42 for stainless steel, titanium, and high-strength alloys at higher cutting speeds; T15 for severe wear and difficult-to-machine materials. Recommended hardness: HRC 62–66.
Q. Which tool steel grade and hardness should I use for cold work dies and hot work molds?
A. Cold work: D2/D3 HRC 58–62; O1/A2 HRC 58–62; S7 HRC 54–58. Hot work: H13/1.2344 HRC 44–52. Plastic molds: P20 HRC 28–34; D2/1.2379 HRC 58–62 for high-wear inserts.


here
for
price